Molded Pulp Egg Cartons

Every egg you sell arrives in something. Our molded pulp egg cartons are formed from 100% recycled paper fiber into cartons that protect the eggs, carry your brand, and break down in a home compost pile when the customer is finished with them. No plastic, no foam, no coating.

Here is what the range gives you:

  • Every count you need. Four, six, ten, twelve, eighteen, and twenty cell layouts running on molds we already own, so most orders skip the tooling charge entirely.
  • Cut for the bird, not just the count. Chicken cells shaped to the USDA weight grades and quail cells cut to true quail diameter, because a small egg in a large cup is an egg that chips.
  • Color that runs through the fiber. Pigment blended into the pulp before forming, not sprayed on after. Scuff the carton and the color underneath is the same.
  • Your brand pressed into the mold. Embossed and debossed lids cost nothing per unit once the tool exists, and there is no ink to scuff or label to peel in a cold room.
  • Freight that works in your favor. Cartons nest flat, so a container carries far more units than the same order in rigid plastic clamshells.
Colored egg cartons in six pulp shades stacked showing pink, blue, green, purple, yellow, and natural

Material :

Recycled Paper
Packaging :
Egg Carton
Process :
Wet Press
Color :
Multicolor

Material :

Recycled paper
Packaging :
Egg Carton
Process :
Wet Press
Color :
Natural

Material :

Recycled Paper
Packaging :
Quail Egg Carton
Process :
Wet Press
Color :
Natural

Material :

Material type
Packaging :
Packaging type
Process :
Process list
Color :
Color Gray
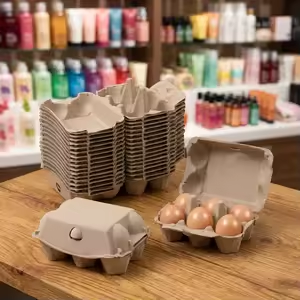
Dozen egg carton in molded pulp open to show twelve brown eggs seated in cells

Material :

Material type
Packaging :
Packaging type
Process :
Process list
Color :
Color Gray

Material :

Material type
Packaging :
Packaging type
Process :
Process list
Color :
Color Gray

Our Product Categories

Discover Bonitopak’s diverse range of packaging solutions, including molded pulp trays, food packaging, custom designs, and sustainable options. Each category is crafted for durability, functionality, and environmental responsibility, tailored to meet your specific needs.

Two ways to color a pulp carton, and only one of them lasts

Colored egg cartons are produced by two very different methods, and the difference determines almost everything about how the finished carton performs.

Surface coating applies pigment after the carton is formed and dried, either by spray or by print. It is cheap, it allows fast color changes, and it produces bright results. It also sits on top of the fiber. Scuff a coated carton against a shelf edge and the natural pulp shows through. Coating also adds a layer that may not compost at the same rate as the fiber underneath, which undermines the reason most buyers chose pulp.

Wet end pigmentation blends the pigment into the pulp slurry before the mold ever touches it. The color is distributed through the fiber, so a torn edge shows the same shade as the face. Nothing can scuff off because there is no layer to remove.

Bonitopak colors at the wet end. That is why our colored cartons cost more than a coated equivalent and why they still look correct after a shipping cycle.

What pigment does to compostability

The concern buyers raise most often is whether color compromises the environmental claim. It is a fair question and the answer depends entirely on pigment selection.

Pigments intended for packaging that will compost have to break down without leaving heavy metals or persistent residue in the finished compost. That rules out several traditional colorant chemistries, particularly some historic reds and yellows. It leaves a narrower palette, which is one reason pulp color ranges are smaller than plastic ones.

Working inside that constraint, a pigmented pulp carton composts on essentially the same timeline as a natural one. The fiber is the same, the quantity of pigment is very small by mass, and there is no film or coating to interfere.

Buyers should ask any colored pulp supplier which pigment system they use and whether it is rated for compostable packaging. A supplier who cannot answer is probably surface coating.

Batch consistency is the real production challenge

Getting a color right once is straightforward. Getting the same color across a twelve month supply relationship is where suppliers separate.

Recycled pulp is not a consistent starting point. Incoming fiber varies in base color depending on the waste stream, seasonally and by supplier. A pigment dose that produces the target shade on a light batch will produce something darker on a gray one.

The control is measurement rather than recipe. Base pulp brightness is checked before dosing, the pigment quantity is adjusted against that reading, and formed samples are compared to a retained physical standard rather than to a color chip on a screen. Records for each batch let a repeat order be matched to the original rather than to the nominal specification.

Buyers running a branded line should request a retained sample at first production and reference it on every reorder. It is the only reliable way to hold a shade over time.

Where color earns its cost

Color adds cost. It is worth understanding where it pays that back.

At a farm stand or market table, a colored carton separates one producer from every other producer selling the same product in gray pulp. That visual difference does more work than any label, because it registers before the shopper is close enough to read anything.

In retail, color functions as a range signal. Producers commonly use different shades to distinguish free range from pasture raised, or standard from organic, which lets a shopper find their usual product without reading the pack.

In gift and seasonal channels, color is the product. Easter, holiday hampers, and branded corporate gifts are bought on appearance.

Where color rarely pays back is commodity commercial packing. If eggs are going through a grading station to a retailer who applies their own labeling, the carton is invisible and natural pulp is the right call.

Specifying color across a range

Buyers running several cell counts in one brand color need to plan for it, because each mold is a separate production run and shade drift between molds is a genuine risk.

The reliable approach is to run all molds in the same color from the same pigment batch where volumes allow, or to match every mold to one retained physical standard where they cannot. Ordering a dozen egg carton and a 6 egg carton in the same shade six months apart without a retained standard will usually produce a visible difference.

Buyers focused on a single shade should see pink egg cartons for the shade specific detail. Those pairing color with a distinctive shape should look at octagon egg cartons or vintage egg cartons.
Colored egg cartons are produced by two very different methods, and the difference determines almost everything about how the finished carton performs.

Surface coating applies pigment after the carton is formed and dried, either by spray or by print. It is cheap, it allows fast color changes, and it produces bright results. It also sits on top of the fiber. Scuff a coated carton against a shelf edge and the natural pulp shows through. Coating also adds a layer that may not compost at the same rate as the fiber underneath, which undermines the reason most buyers chose pulp.

Wet end pigmentation blends the pigment into the pulp slurry before the mold ever touches it. The color is distributed through the fiber, so a torn edge shows the same shade as the face. Nothing can scuff off because there is no layer to remove.

Bonitopak colors at the wet end. That is why our colored cartons cost more than a coated equivalent and why they still look correct after a shipping cycle.

What pigment does to compostability

The concern buyers raise most often is whether color compromises the environmental claim. It is a fair question and the answer depends entirely on pigment selection.

Pigments intended for packaging that will compost have to break down without leaving heavy metals or persistent residue in the finished compost. That rules out several traditional colorant chemistries, particularly some historic reds and yellows. It leaves a narrower palette, which is one reason pulp color ranges are smaller than plastic ones.

Working inside that constraint, a pigmented pulp carton composts on essentially the same timeline as a natural one. The fiber is the same, the quantity of pigment is very small by mass, and there is no film or coating to interfere.

Buyers should ask any colored pulp supplier which pigment system they use and whether it is rated for compostable packaging. A supplier who cannot answer is probably surface coating.

Batch consistency is the real production challenge

Getting a color right once is straightforward. Getting the same color across a twelve month supply relationship is where suppliers separate.

Recycled pulp is not a consistent starting point. Incoming fiber varies in base color depending on the waste stream, seasonally and by supplier. A pigment dose that produces the target shade on a light batch will produce something darker on a gray one.

The control is measurement rather than recipe. Base pulp brightness is checked before dosing, the pigment quantity is adjusted against that reading, and formed samples are compared to a retained physical standard rather than to a color chip on a screen. Records for each batch let a repeat order be matched to the original rather than to the nominal specification.

Buyers running a branded line should request a retained sample at first production and reference it on every reorder. It is the only reliable way to hold a shade over time.

Where color earns its cost

Color adds cost. It is worth understanding where it pays that back.

At a farm stand or market table, a colored carton separates one producer from every other producer selling the same product in gray pulp. That visual difference does more work than any label, because it registers before the shopper is close enough to read anything.

In retail, color functions as a range signal. Producers commonly use different shades to distinguish free range from pasture raised, or standard from organic, which lets a shopper find their usual product without reading the pack.

In gift and seasonal channels, color is the product. Easter, holiday hampers, and branded corporate gifts are bought on appearance.

Where color rarely pays back is commodity commercial packing. If eggs are going through a grading station to a retailer who applies their own labeling, the carton is invisible and natural pulp is the right call.

Specifying color across a range

Buyers running several cell counts in one brand color need to plan for it, because each mold is a separate production run and shade drift between molds is a genuine risk.

The reliable approach is to run all molds in the same color from the same pigment batch where volumes allow, or to match every mold to one retained physical standard where they cannot. Ordering a dozen egg carton and a 6 egg carton in the same shade six months apart without a retained standard will usually produce a visible difference.

Buyers focused on a single shade should see pink egg cartons for the shade specific detail. Those pairing color with a distinctive shape should look at octagon egg cartons or vintage egg cartons.

Two ways to color a pulp carton, and only one of them lasts

Colored egg cartons are produced by two very different methods, and the difference determines almost everything about how the finished carton performs.

Surface coating applies pigment after the carton is formed and dried, either by spray or by print. It is cheap, it allows fast color changes, and it produces bright results. It also sits on top of the fiber. Scuff a coated carton against a shelf edge and the natural pulp shows through. Coating also adds a layer that may not compost at the same rate as the fiber underneath, which undermines the reason most buyers chose pulp.

Wet end pigmentation blends the pigment into the pulp slurry before the mold ever touches it. The color is distributed through the fiber, so a torn edge shows the same shade as the face. Nothing can scuff off because there is no layer to remove.

Bonitopak colors at the wet end. That is why our colored cartons cost more than a coated equivalent and why they still look correct after a shipping cycle.

What pigment does to compostability

The concern buyers raise most often is whether color compromises the environmental claim. It is a fair question and the answer depends entirely on pigment selection.

Pigments intended for packaging that will compost have to break down without leaving heavy metals or persistent residue in the finished compost. That rules out several traditional colorant chemistries, particularly some historic reds and yellows. It leaves a narrower palette, which is one reason pulp color ranges are smaller than plastic ones.

Working inside that constraint, a pigmented pulp carton composts on essentially the same timeline as a natural one. The fiber is the same, the quantity of pigment is very small by mass, and there is no film or coating to interfere.

Buyers should ask any colored pulp supplier which pigment system they use and whether it is rated for compostable packaging. A supplier who cannot answer is probably surface coating.

Batch consistency is the real production challenge

Getting a color right once is straightforward. Getting the same color across a twelve month supply relationship is where suppliers separate.

Recycled pulp is not a consistent starting point. Incoming fiber varies in base color depending on the waste stream, seasonally and by supplier. A pigment dose that produces the target shade on a light batch will produce something darker on a gray one.

The control is measurement rather than recipe. Base pulp brightness is checked before dosing, the pigment quantity is adjusted against that reading, and formed samples are compared to a retained physical standard rather than to a color chip on a screen. Records for each batch let a repeat order be matched to the original rather than to the nominal specification.

Buyers running a branded line should request a retained sample at first production and reference it on every reorder. It is the only reliable way to hold a shade over time.

Where color earns its cost

Color adds cost. It is worth understanding where it pays that back.

At a farm stand or market table, a colored carton separates one producer from every other producer selling the same product in gray pulp. That visual difference does more work than any label, because it registers before the shopper is close enough to read anything.

In retail, color functions as a range signal. Producers commonly use different shades to distinguish free range from pasture raised, or standard from organic, which lets a shopper find their usual product without reading the pack.

In gift and seasonal channels, color is the product. Easter, holiday hampers, and branded corporate gifts are bought on appearance.

Where color rarely pays back is commodity commercial packing. If eggs are going through a grading station to a retailer who applies their own labeling, the carton is invisible and natural pulp is the right call.

Specifying color across a range

Buyers running several cell counts in one brand color need to plan for it, because each mold is a separate production run and shade drift between molds is a genuine risk.

The reliable approach is to run all molds in the same color from the same pigment batch where volumes allow, or to match every mold to one retained physical standard where they cannot. Ordering a dozen egg carton and a 6 egg carton in the same shade six months apart without a retained standard will usually produce a visible difference.

Buyers focused on a single shade should see pink egg cartons for the shade specific detail. Those pairing color with a distinctive shape should look at octagon egg cartons or vintage egg cartons.

Industry Expertise at BonitoPak

Having produced millions of parts, BonitoPak holds deep knowledge in numerous applications. We excel particularly in industries requiring precise and intricate component fabrication. Trust us to deliver expertise and quality, no matter the complexity.
Ready to Elevate Your Project?

Bring Your Designs to Life with BonitoPak

Experience precision engineering with BonitoPak. From detailed prototypes to high-volume production, we’re here to turn your concepts into reality. Contact us today to discuss your project needs!

Why Choose BonitoPak?

At Bonitopak, we offer customizable, eco-friendly packaging solutions with expert support, sustainable practices, and guaranteed quality. Our innovative designs and efficient production ensure your packaging stands out while reducing environmental impact.

Quick Solutions

We respond within 24 hours, offering fast, clear communication, tailored solutions, and efficient service to save time and costs.

Swift Adaptability

Our in-house design, engineering, and manufacturing ensure rapid tooling, with samples ready in 7 days and production molds in 8 days.

Expert Innovators

Our skilled R&D engineers excel in designing, prototyping, and tooling, offering complete packaging solutions with blister, tin can, and printed boxes.

Efficient Optimization

Trained staff conduct 100% inspections, random checks, and quality control, ensuring high standards, reducing rejects, and saving costs.

Prompt Delivery

We provide reasonable order scheduling and coordinate with clients to resolve issues promptly, ensuring the best solutions.

Excellent Support

Our experienced after-sales team ensures smooth communication, solving issues with replacements, shipping, and delivery, aiming for zero complaints.

Related Articles and Insights

Stay informed with the latest updates on sustainable packaging trends, industry insights, and expert tips through our blog. Explore innovative ideas and solutions to enhance your packaging knowledge.

Canada has a smaller domestic moulded pulp sector than the United States, but it has

Australia has one domestic moulded fibre egg carton manufacturer. Huhtamaki Australia describes itself as the

British egg packaging is sold differently from the American market. Where US suppliers talk in

Frequently Asked Questions

Molded Pulp Colored Egg Cartons

  • Can I get a color card before ordering?

    Yes, and we recommend it. Screen renderings of pulp color are unreliable because fiber texture affects perceived shade. We send physical color chips of the six stock shades, and for custom work we produce a formed sample in the actual carton geometry, since a flat chip and a molded surface read differently.

  • Does the pigment transfer onto the eggshells?

    No. The pigment is bound within the fiber structure, not sitting loose on the surface, and dry pulp does not transfer color under normal handling. A carton that marks the eggs would indicate a surface coated product with poor adhesion, which is one of the practical arguments for wet end coloring.

  • Why do colored cartons cost more than natural?

    Three reasons. The pigment itself is an added material cost. Wet end color changes require the system to be flushed between shades, which is downtime. And colored runs cannot absorb variable incoming fiber the way natural production can, so more batches get rejected on shade. Stock colors cost less than custom because we run them continuously and avoid most of the changeover.

  • Can you match my exact brand color?

    We can get close, and we produce a physical match sample before any full run so you can approve or adjust. Exact matching to a printed Pantone reference is not achievable in pigmented fiber, because pulp scatters light differently than coated paper does. Brands with a strict color standard usually approve a designated pulp equivalent rather than insisting on the ink reference.

  • Will colored cartons fade in sunlight?

    Slowly, and mostly at a farm stand rather than in a cold case. Pulp pigments are less lightfast than printing inks because the palette is limited to compostable chemistries. Cartons held in direct sun for weeks will lighten, particularly in the blue and purple range. Retail cold cases and covered market stalls are not a problem.

Fill This Detailed Form