Explore our wide range of high-quality, eco-friendly packaging solutions designed to meet the unique needs of various industries. From custom designs to sustainable materials, find the perfect packaging option for your product requirements.
Every molded pulp part starts as a fiber slurry, and the fiber chosen at that stage sets the limits on everything that follows. Strength, surface finish, color, food contact suitability, compost behavior, and cost are all decided before the mold closes. BonitoPak runs nine molded pulp packaging materials, and this page explains what each one does so you can specify the right fiber rather than discover it after tooling.
Phase Which Molded Pulp Material Should You Choose?
The molded pulp packaging materials in our range fall into three families. Virgin wood fibers (wood pulp, bleached pulp, compostable kraft paper) give the highest strength and the cleanest appearance at the highest cost. Agricultural residue fibers (straw fiber, natural plant fiber, and bagasse) use material that would otherwise be burned or discarded, at moderate strength and low cost. Recycled fibers (recycled paper pulp, corrugated paper) cost least and carry the strongest circularity story, with shorter fibers and a characteristic gray-brown color. Bamboo fiber sits apart. It is a fast-growing grass rather than a tree or a residue, and it delivers near-virgin-wood strength with a renewability profile closer to agricultural fiber. Colored pulp is not a separate fiber. It is any of the above with pigment blended into the slurry before forming.
The Nine Materials at a Glance
Material
Fiber Source
Avg. Fiber Length
Strength
Finish
Relative Cost
Best For
Compostable Kraft Paper
Virgin softwood
2.5–4.5 mm
Highest
Brown, textured
High
Load-bearing parts, wraps, liners
Bamboo Fiber
Bamboo culm
1.5–3.0 mm
Very High
Pale, fine
Medium–High
Strength with a renewable story
Wood Pulp
Softwood and hardwood
0.8–4.5 mm
High
Smooth, pale
Medium–High
Precision parts, fine detail
Bleached Pulp
Bleached wood or bamboo
0.8–3.0 mm
High
White, smooth
High
Food-contact applications subject to compliance, premium white packaging
Natural Plant Fiber
Mixed plant sources
1.0–2.0 mm
Medium
Natural, varied
Medium
General-purpose packaging
Straw Fiber
Wheat and rice straw
1.0–1.5 mm
Medium
Pale gold, textured
Low
Volume parts, agricultural circularity
Corrugated Paper
Recovered OCC
0.8–1.5 mm
Medium
Brown, coarse
Low
Protective inserts, transit packaging
Recycled Paper Pulp
Post-consumer paper
0.8–1.5 mm
Medium
Gray-brown
Lowest
Egg packaging, high-volume inserts
Colored Pulp
Any base plus pigment
Follows base fiber
Follows base
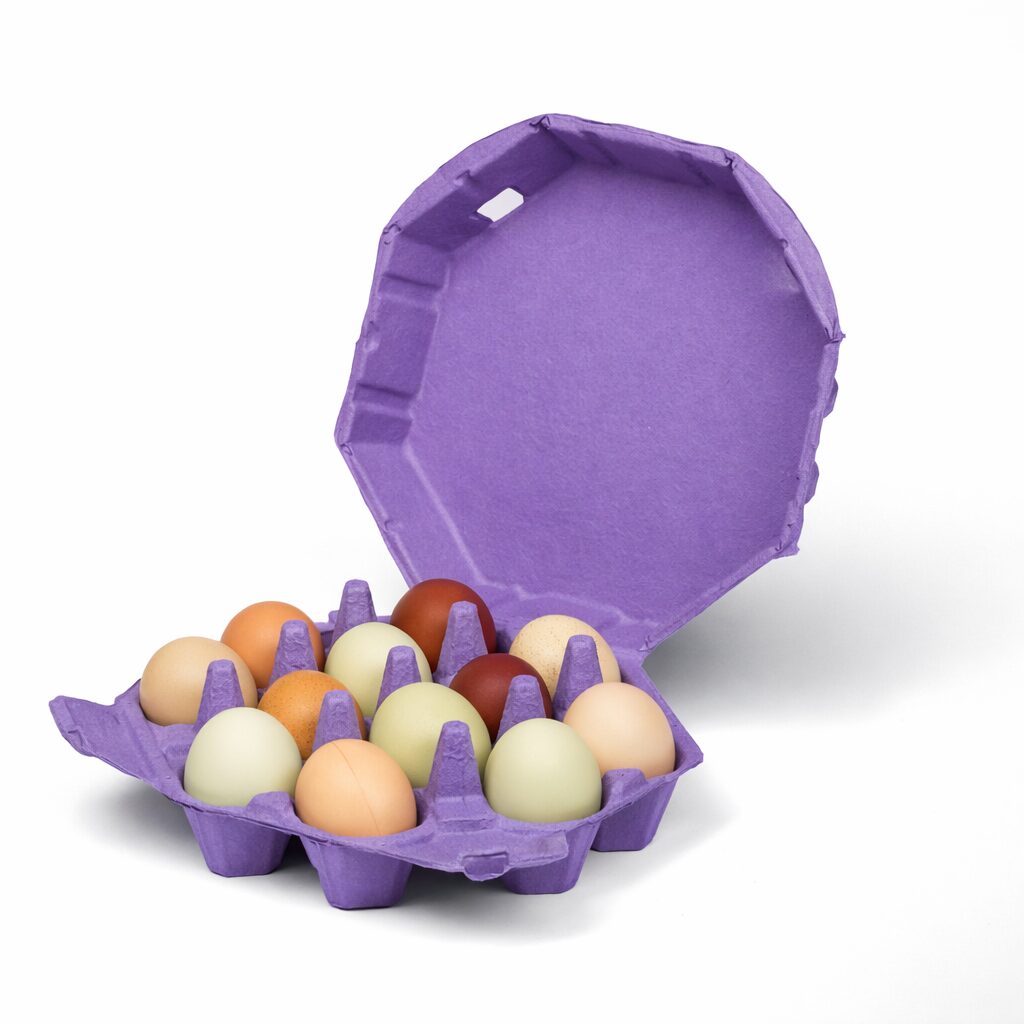
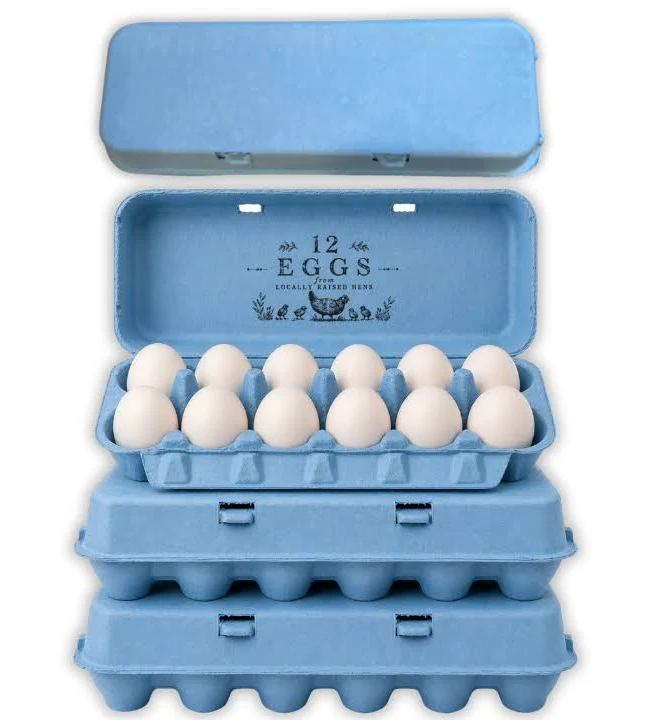
Custom colors
Base plus pigment
Branded and retail-facing packaging
Understanding Molded Pulp Materials
Why Fiber Length Decides Almost Everything
If you learn one thing about molded pulp materials, make it this: fiber length determines strength, and almost every other property follows from the same trade.
Long fibers interlock. A softwood kraft fiber at 3 mm bridges across many neighboring fibers and transfers load through the network, which is why kraft-based parts resist tearing and carry compression. Short fibers, around 1 mm, bond at fewer points, so the same wall thickness carries less load.
Short fibers have their own advantage. They flow into mold detail that long fibers bridge over, and they drain more predictably on the forming screen, which gives better dimensional consistency and a finer surface. This is why recycled paper pulp, with its short degraded fibers, is the dominant material in egg packaging where detail and consistency matter more than tensile strength.
Most production furnishes are blends for exactly this reason. A proportion of long fiber provides the structural network while short fiber fills detail and smooths the surface. When we specify a material for a part, we are usually specifying a ratio rather than a single source.
The Four Molded Pulp Types, and Why the Material Has to Match
The industry classifies molded pulp into four types, and the right fiber differs for each.
Type 1, thick wall. Walls from 1.5 to 6 mm, formed from coarse slurries, rough on one face. Used for edge protectors, heavy item cradles, and pallet trays. Recycled and corrugated fiber suit this type because surface quality is irrelevant and cost dominates.
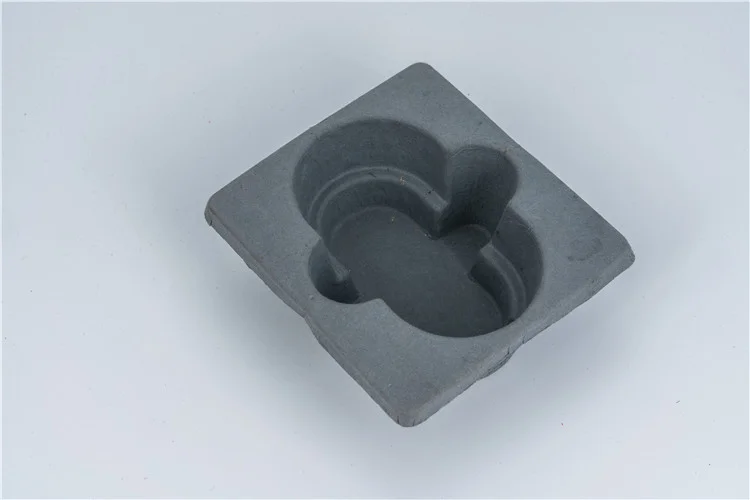
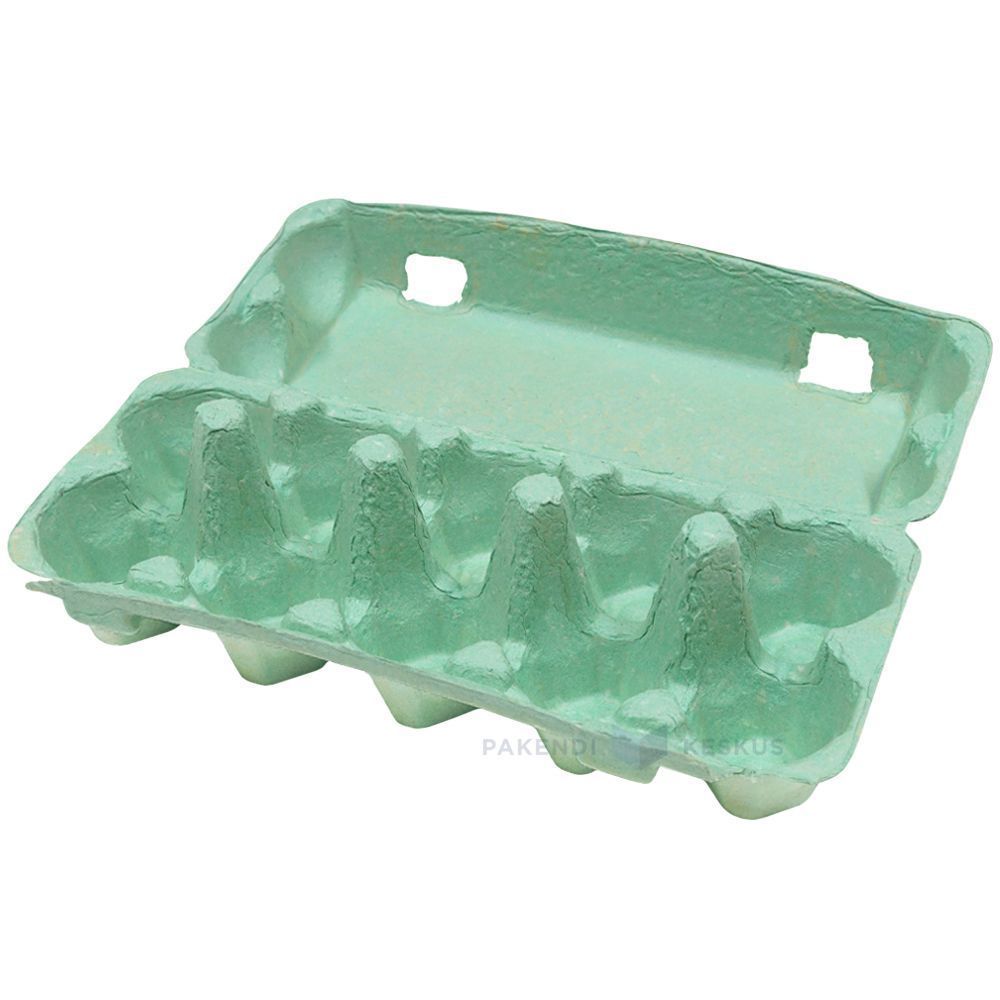
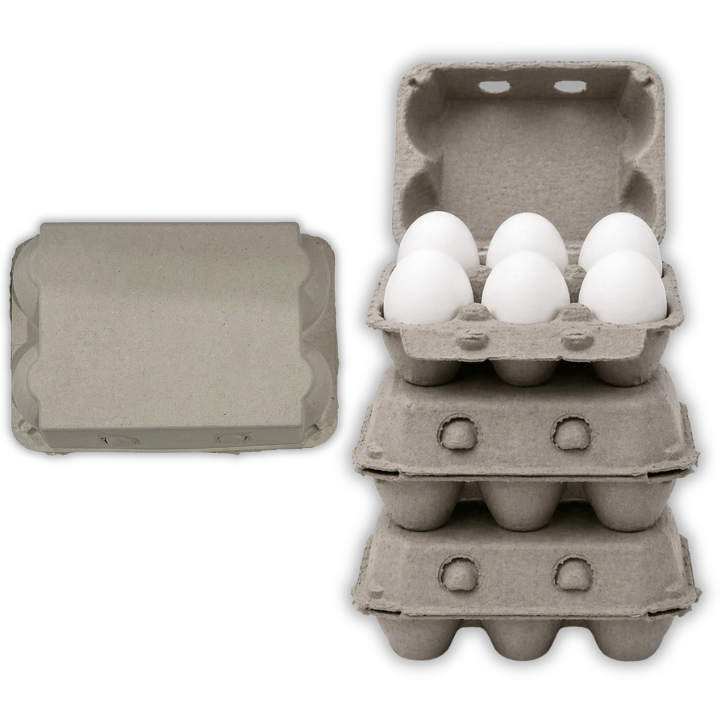
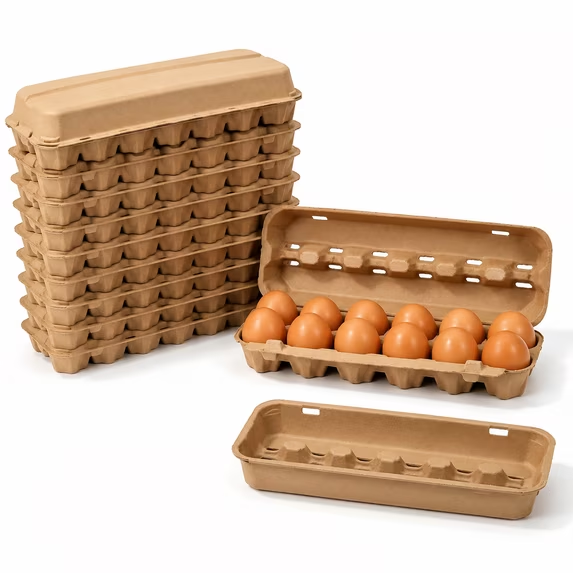
Type 2, transfer molded. Walls roughly 1.6 to 4.8 mm, relatively smooth on one face, with good definition. This covers egg cartons, drink trays, cup carriers, and electronics inserts. Recycled paper pulp and straw fiber are standard here.
Type 3, thermoformed fiber. The newest process, using cure-in-the-mold tooling where heated molds press and densify the part so it ejects finished rather than oven dried. It produces a smooth, well-defined, almost plastic-like surface. Bleached pulp, bamboo, and wood pulp are the materials that justify this process, because the finish is the point.
Type 4, processed. Any of the above with secondary operations: coating, printing, hot pressing, die cutting, or coloring. Colored pulp and printed parts sit here.
Specifying a premium fiber for a Type 1 part wastes money. Specifying recycled fiber for a Type 3 part wastes the process. Matching the two is most of what material selection actually is.
Compostability, Recyclability, and the Difference That Matters
Buyers frequently use the two words interchangeably, and they describe different end-of-life routes with different requirements.
Compostable means the material breaks down into water, carbon dioxide, and biomass within a defined period under defined conditions, leaving no toxic residue. The governing standards are EN 13432 in Europe and ASTM D6400 and D6868 in North America. Certification marks include OK Compost and BPI. Uncoated molded pulp from any of our nine materials generally meets the chemistry requirement, because it is cellulose with nothing added.
Recyclable means the material can re-enter a paper recycling stream. Here fiber length works against pulp. Fibers in recycled paper pulp have already been through several cycles and are near the end of their usable life, which is why some municipal programs direct molded pulp to compost rather than to paper.
The practical consequence is that coating changes everything. A barrier coating applied for grease or moisture resistance can disqualify an otherwise compostable part. We do not apply plastic barrier coatings, which is the reason our parts stay in the single-material category.
Food Contact, and What Actually Governs It
Food contact suitability is a regulatory question rather than a material quality question, and it varies by market.
In the United States, FDA 21 CFR 176.170 governs paper and paperboard components in contact with aqueous and fatty foods. In the European Union, Regulation 10/2011 and the relevant national measures apply, with Germany’s BfR Recommendation XXXVI commonly referenced for paper.
What matters in practice: the fiber source, whether recycled content is permitted for the specific food type, and whether any process chemistry carries over into the finished part. Bleached pulp is the usual specification for direct food contact because it is virgin fiber with controlled chemistry. Recycled fiber is restricted for direct contact with many food types in several markets.
Eggs are a useful edge case. The shell is the food contact surface, so egg packaging is generally treated as secondary rather than primary packaging, which is why recycled fiber dominates it.
How We Select a Material With You
Choosing between molded pulp packaging materials comes down to four questions, in this order.
What does the part have to survive? Compression in a pallet stack, drop impact, or neither. This sets the fiber length requirement.
Who sees it? A transit insert nobody opens can be gray recycled fiber. A retail unit or an unboxing experience needs finish, which pushes toward bleached, bamboo, or wood pulp.
Does it touch food? If yes, the market and the food type narrow the options immediately.
What is the cost ceiling? The blend ratio gets decided here, because the usual answer is some long fiber for structure and some short fiber for everything else.
Send us the product, the drawing, or the problem and we will work through those four with you. Where molded pulp is the wrong material entirely, we say so.
Explore Bonitopak’s range of sustainable, high-quality packaging solutions, including molded pulp trays, eco-friendly food containers, and custom-designed packaging. Each product is crafted to meet your unique needs while promoting environmental responsibility and exceptional functionality.
Experience precision engineering with BonitoPak. From detailed prototypes to high-volume production, we’re here to turn your concepts into reality. Contact us today to discuss your project needs!
At Bonitopak, we offer customizable, eco-friendly packaging solutions with expert support, sustainable practices, and guaranteed quality. Our innovative designs and efficient production ensure your packaging stands out while reducing environmental impact.
Quick Solutions
We respond within 24 hours, offering fast, clear communication, tailored solutions, and efficient service to save time and costs.
Swift Adaptability
Our in-house design, engineering, and manufacturing ensure rapid tooling, with samples ready in 7 days and production molds in 8 days.
Expert Innovators
Our skilled R&D engineers excel in designing, prototyping, and tooling, offering complete packaging solutions with blister, tin can, and printed boxes.
Efficient Optimization
Trained staff conduct 100% inspections, random checks, and quality control, ensuring high standards, reducing rejects, and saving costs.
Prompt Delivery
We provide reasonable order scheduling and coordinate with clients to resolve issues promptly, ensuring the best solutions.
Excellent Support
Our experienced after-sales team ensures smooth communication, solving issues with replacements, shipping, and delivery, aiming for zero complaints.
Frequently Asked Questions (FAQs)
What is molded pulp packaging made of?
A slurry of water and cellulose fiber, vacuum formed against a screen mold and dried. The fiber comes from wood, bamboo, agricultural residue such as wheat or rice straw, or recovered paper. Nothing else is required. Pigments, and occasionally sizing agents for moisture resistance, are the only common additions, and both are selected to keep the part compostable.
Which molded pulp material is strongest?
Compostable kraft paper, because virgin softwood gives the longest fibers at 2.5 to 4.5 mm and the longest fibers build the strongest bonded network. Bamboo is close behind and carries a better renewability profile. If your part has to carry compression in a deep pallet stack, those two are where to start.
Is molded pulp packaging waterproof?
Not inherently. Cellulose absorbs water, which is useful for products like eggs that benefit from moisture regulation, and a problem for wet or greasy contents. Water resistance is added through sizing agents in the slurry or barrier coatings applied afterward. Coatings improve performance and can compromise compostability, so the trade needs deciding at specification rather than later.
Can molded pulp replace expanded polystyrene foam?
In most protective packaging applications, yes. Pulp matches foam on compression and transit protection for the majority of products and beats it on disposal, nesting efficiency, and freight volume. Foam still wins where extreme lightness or very high impact absorption at low density is essential. We make pulp rather than foam, so we would rather state that limit plainly than claim pulp wins on every measure.
How long does molded pulp take to compost?
Uncoated pulp typically breaks down within 30 to 90 days in a commercial composting facility and takes longer in a home pile, depending on moisture, temperature, and how finely the material is broken up. Standards such as EN 13432 and ASTM D6400 define the test conditions and the thresholds, which is why certification references a standard rather than a single number of days.
Related Articles and Insights
Stay informed with the latest updates on sustainable packaging trends, industry insights, and expert tips through our blog. Explore innovative ideas and solutions to enhance your packaging knowledge.