漂白パルプ

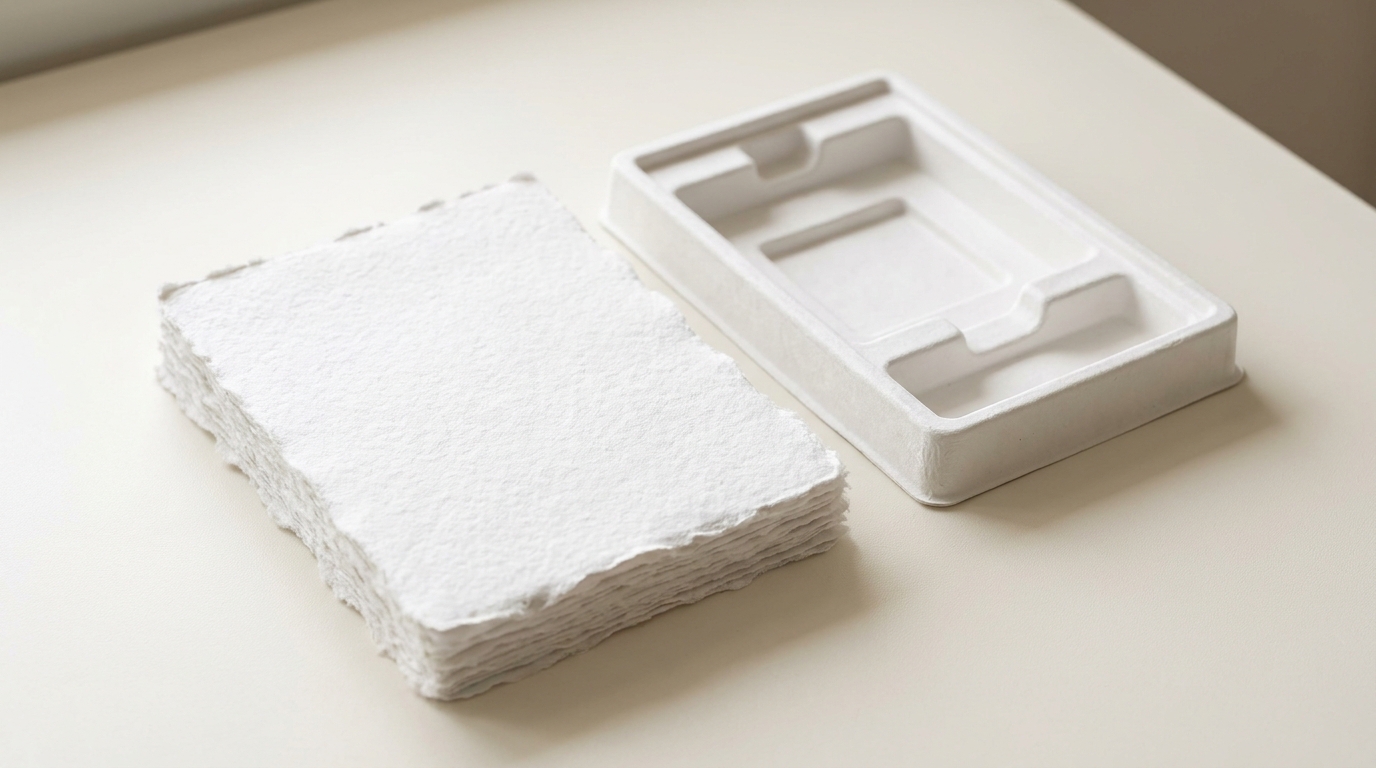
Bleached pulp is the material to specify when the part has to be white, has to touch food, or has to look like a finished product rather than packaging. We bleach with hydrogen peroxide rather than chlorine, which is a totally chlorine free route that leaves no chlorinated organic residue in the fiber or the effluent. The result is a clean white virgin fiber with controlled chemistry, which is what food contact compliance actually requires.
Why bleached pulp is the food contact default

Totally chlorine free bleaching. Hydrogen peroxide breaks down into water and oxygen, leaving no chlorinated organic compounds in the fiber. This is the TCF route rather than the ECF route that uses chlorine dioxide.
Virgin fiber with known history. Recycled fiber carries whatever was in the paper it came from, which is why many markets restrict it for direct food contact. Virgin fiber has a traceable chemistry.
White base for accurate color. Pigment applied over a white base reproduces predictably, where the same pigment over gray-brown recycled fiber shifts with every batch of incoming fiber.
Smooth surface for Type 3 forming. This material justifies cure-in-the-mold tooling, where heated molds press and densify the part to a smooth, well-defined, almost plastic-like finish.
Premium appearance without coating. White reads as finished and clinical, which suits cosmetics, medical, and premium retail without adding any surface layer.
Compostable on the same basis as unbleached. Peroxide bleaching removes lignin and brightens cellulose. It does not introduce anything that interferes with breakdown.
Bleaching is a lignin removal and brightening process, not a coating. Residual lignin is what makes unbleached kraft brown, and peroxide oxidizes the chromophores responsible for that color. Some fiber strength is lost in the process, which is the main trade: a bleached part is marginally weaker than the same fiber unbleached, at the same wall thickness.
That trade is worth making whenever appearance or compliance is the driver, and not worth making for a transit insert nobody sees.

Specification table

仕様 詳細
材料名 漂白パルプ
素材タイプ Virgin fiber, hydrogen peroxide bleached
繊維源 Softwood, hardwood, or bamboo
Average Fiber Length 0.8 to 3.0 mm depending on source
Bleaching Method Totally chlorine free, hydrogen peroxide
Chlorinated Residue なし
Natural Color ホワイト
表面仕上げ Smooth, suitable for Type 3 thermoformed fiber
Relative Strength High; marginally below unbleached equivalent
Typical Wall Thickness 0.8 to 3.0 mm
プロセスの互換性 Wet pressing, dry pressing, thermoformed fiber
成形パルプの種類 Type 2, Type 3, Type 4
食品との接触 Preferred base; confirm against FDA 21 CFR 176.170 or EU 10/2011
堆肥化可能性 Meets the chemistry basis for EN 13432 and ASTM D6400 uncoated
カラーオプション White base; takes pigment with the highest accuracy in the range
相対コスト 高い
認証 FSC or PEFC chain of custody available on request

Where bleached pulp earns its premium

Direct food contact. Where the part touches food rather than sitting outside a sealed product, bleached virgin fiber is the specification that clears regulatory review most easily in most markets. Trays for produce, confectionery inserts, and food service items all sit here.
Cosmetics and personal care. A white insert inside a gift set or a skincare box reads as part of the product. Brands moving away from vacuum-formed plastic trays usually land here, because it is the only fiber that matches the finish expectation.
Medical and pharmaceutical. White is the convention in this sector, and virgin fiber with controlled chemistry is the baseline requirement. Single-use hospital disposables are among the oldest molded pulp applications.
Any part being pigmented to a precise shade. The white base removes the variability that makes color matching difficult on recycled fiber. If a brand color has to reproduce exactly across years of reorders, starting from bleached fiber is the most reliable route. See colored pulp for how that process works.
Where bleached pulp is the wrong call: protective transit packaging where appearance is irrelevant, and any cost-driven volume part. For those, recycled paper pulp or straw fiber deliver the function at a fraction of the material cost.
Buyers who want a pale finish without a bleaching stage should look at bamboo fiber, which forms naturally paler than wood and considerably paler than recycled fiber.

よくある質問 (FAQ)

Is bleached pulp treated with chlorine?
Not in our process. We use hydrogen peroxide, which is the totally chlorine free route. The alternative industry route, elemental chlorine free, uses chlorine dioxide and is still widely practiced, but it produces chlorinated organic compounds that TCF avoids entirely. If chlorine chemistry is a procurement requirement for you, this distinction is worth confirming with any supplier.
Peroxide bleaching adds an energy and chemical input, and it decomposes into water and oxygen rather than persisting. The part remains compostable and uncoated. The honest comparison is that it carries a higher processing footprint than unbleached fiber and a lower one than any plastic alternative it replaces, and that it is worth specifying when appearance or compliance requires it rather than by default.
The bleaching stage removes residual lignin and acts on the cellulose chains, which shortens some fibers and reduces bonding slightly. The loss is modest and usually irrelevant at the wall thicknesses these parts run at. For a part where maximum strength is the governing requirement, compostable kraft paper is the better specification.
No. Uncoated cellulose absorbs water regardless of bleaching, so these are single-use parts for dry or briefly-contacted contents. Hot or wet applications need a barrier, and barrier coatings generally compromise compostability. If your application involves sustained liquid contact, tell us at quotation so we can say whether pulp is viable at all.
Slowly, under ultraviolet light and in high heat, which is a normal property of cellulose rather than a defect in bleaching. Parts stored in dark warehouse conditions stay white for practical purposes. Parts in a sunlit retail display will warm in tone over months. Brightness stabilizers exist but need checking against food contact and compostability for your market before use.
材料名

漂白パルプ

素材タイプ

環境に優しい晒し繊維

プロセスの互換性

ボニトパック包装資材

当社のパッケージング・ソリューションは、サトウキビ繊維、竹、再生紙パルプなどの持続可能な素材から作られており、さまざまな製品に環境に優しく生分解性のオプションを提供しています。

生分解性クラフト紙は、当社が製造する繊維製品の中で最も強度が高いものです。バージン

着色パルプは、独立した繊維ではありません。これは、当社の

部品が以下の条件を満たす必要がある場合は、漂白パルプを指定する必要があります。

天然植物繊維とは、当社がブレンドに用いる、木材以外のセルロース源を指します。

成形パルプ材料としての段ボール紙とは、回収された段ボール箱を再パルプ化したものを指す。

わら繊維は、穀物の収穫後に残る茎から作られる素材です。

製品カテゴリー

成型パルプトレイ、食品包装、カスタムデザイン、持続可能なオプションなど、Bonitopakの多様なパッケージングソリューションをご覧ください。各カテゴリーは、耐久性、機能性、環境への責任を考慮し、お客様の特定のニーズに合わせて作られています。
あなたのプロジェクトを向上させる準備はできていますか?

BonitoPakでデザインに命を吹き込もう

BonitoPakで精密なエンジニアリングを体験してください。詳細なプロトタイプから大量生産まで、お客様のコンセプトを現実にします。今すぐお問い合わせください!

関連記事と洞察

持続可能なパッケージングのトレンド、業界の洞察、専門家のヒントに関する最新情報をブログでお届けします。革新的なアイデアやソリューションを探求し、パッケージングの知識を深めましょう。

レオ・チャン | BonitoPak ライター | 成形パルプ包装業界で20年以上の経験を持つ ウォッカとは

レオ・チャン | BonitoPak ライター | 成形パルプ包装業界で20年以上の経験 ほぼすべての

レオ・チャン | BonitoPak ライター | 成形パルプ包装分野で20年以上の経験 検索

詳細フォーム