Farbiger Zellstoff

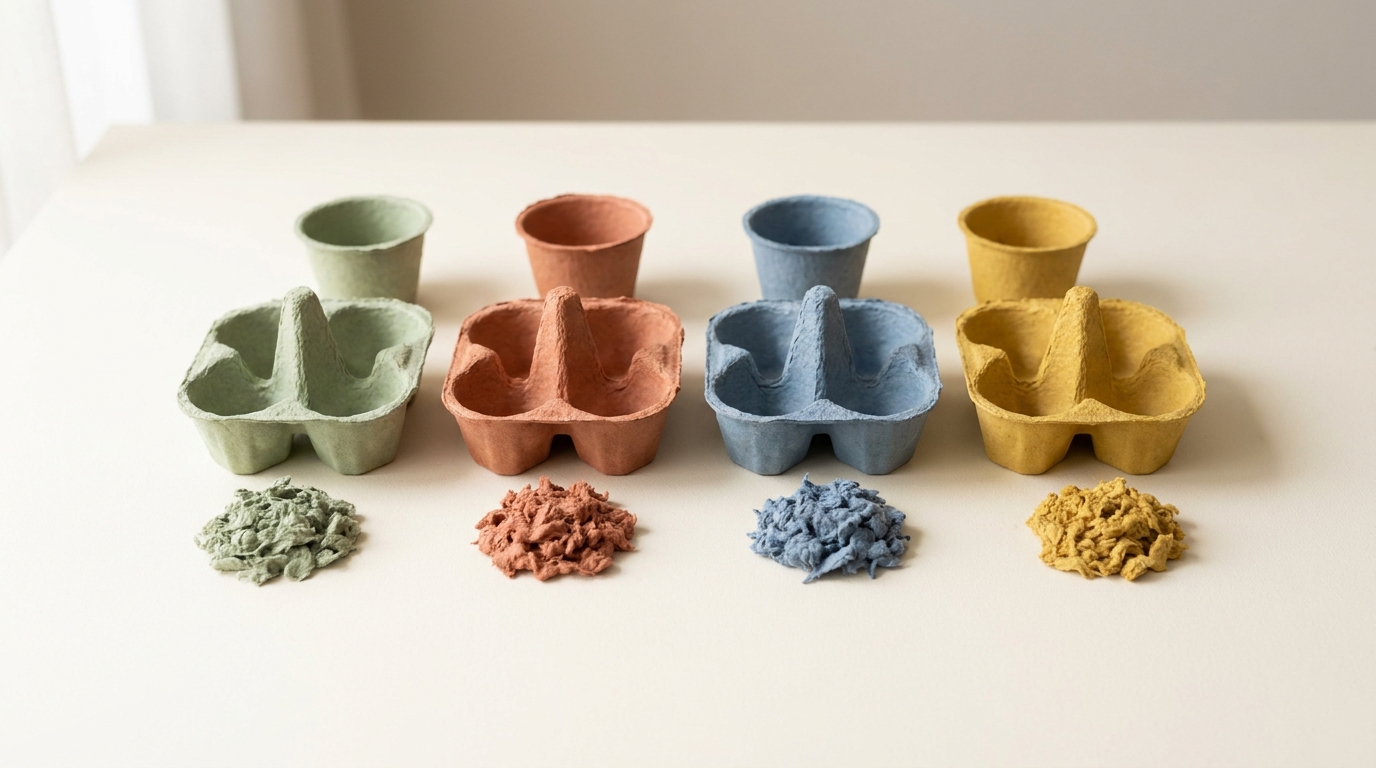
Colored pulp is not a separate fiber. It is any of our base materials with pigment blended into the slurry before the mold ever touches it, so the color runs through the full depth of the fiber wall. Scuff the surface and the color underneath is identical. That is the difference between pigmented pulp and coated pulp, and it is why a colored part still looks correct after a shipping cycle.
Why wet end pigmentation beats surface coating

  • The color is the material. Pigment is dispersed through the slurry, so a torn edge shows the same shade as the face. There is no layer to scuff, chip, or peel.
  • Compostability is unchanged. Pigments are selected to meet the same breakdown requirements as the fiber, and they are present in very small quantity by mass. No coating is introduced.
  • No transfer onto contents. Bound pigment does not rub off. Surface-coated parts with weak adhesion can mark the product they hold.
  • Six stock shades held in production. Running continuously, which means lower minimums and no changeover premium compared with a custom match.
  • Custom matching against a physical sample. We produce a formed sample in your actual part geometry for approval, because a flat chip and a molded surface read differently.
  • Darker shades sharpen embossing. Embossed detail reads through shadow rather than contrast, and darker pigment holds shadow more cleanly at the edge of the mark.

The constraint worth understanding is the palette. Pigments used in compostable packaging have to break down without leaving heavy metals or persistent residue, which rules out several traditional colorant chemistries, particularly in the red and yellow ranges. The result is a narrower palette than plastic offers. Within it, the range covers most brand requirements.

The second constraint is the base. Recycled fiber arrives gray-brown and varies batch to batch with the waste stream. Every pigment works against that moving base. Dark shades overwhelm it and reproduce consistently. Light tints show it, which is why pale pink and pale lavender are the hardest shades in the range to hold across reorders and why a retained physical standard matters for them.

Specification table

Spezifikation Einzelheiten
Material Name Farbiger Zellstoff
Material Typ Base fiber with slurry-blended pigment
Base Fiber Options Recycled, bleached, bamboo, straw, wood, plant fiber
Coloring Method Wet end pigmentation, not surface coating
Color Penetration Full fiber wall depth
Stock Shades Six held in continuous production
Custom Color Pantone reference or physical sample matching
Color Accuracy Approved against a retained physical standard
Lightfastness Dark shades highest; pale tints lowest
Oberflächenbehandlung Follows base fiber
Stärke Follows base fiber; pigment does not affect it
Prozess-Kompatibilität Wet pressing, dry pressing, transfer molding
Geformte Zellstofftypen Type 2, Type 3, Type 4
Kompostierbarkeit Unchanged from base fiber
Food Contact Pigment selection must be confirmed for the specific market
Relative Kosten Base fiber cost plus pigment and changeover

Holding a color across a supply relationship

Getting a shade right once is straightforward. Getting the same shade twelve months later is where suppliers separate, and the control is measurement rather than recipe.

Base pulp brightness is read before pigment dosing, and the dose is adjusted against that reading rather than against a fixed formula. Formed samples are compared against a retained physical standard, not against a color chip on a screen, because fiber texture changes how a shade reads. Batch records let a reorder be matched to the original rather than to the nominal specification.

Any buyer building a brand on a specific color should approve and retain a physical standard at first production. It is the single most useful step available, and it is the difference between cartons that look identical on a shelf and cartons that visibly differ by run.

Lightfastness varies by shade and is worth planning around. Blue and purple pigments rated for compostable use are the least lightfast group, because the chemistries that give strong color without heavy metals are inherently more UV-sensitive. Dark shades hold up longest. In refrigerated retail or indoor display none of this is visible. For outdoor market selling, specify toward the darker end or keep stock covered between days.

Colored pulp runs on any base in our range, so the fiber decision comes first and the color decision second. For the strength and finish characteristics of each base, start at the molded pulp packaging materials hub, or compare Zellstoff aus Recyclingpapier against natürliche Pflanzenfaser, which are the two most commonly pigmented bases. Colored pulp applies across the product range. For egg packaging specifically, see molded pulp colored egg cartons. For the whitest possible base before pigmenting, see gebleichter Zellstoff, which gives the cleanest and most predictable color reproduction of any base in the range.

Häufig gestellte Fragen (FAQs)

Does adding pigment affect the strength of the part?
No measurably. Pigment is present in very small quantity by mass and does not interfere with fiber bonding, which is what carries load. A colored part and a natural part formed from the same furnish at the same wall thickness perform the same in compression. Strength follows the base fiber you select, not the color.
Pulp scatters light differently from coated paper, so an ink reference and a fiber surface cannot produce the same visual result even with identical pigment. We get close and send a formed physical sample for approval. Brands with a strict standard generally approve a designated pulp equivalent alongside their print reference rather than requiring the two to match.
Yes, through custom matching. It carries a higher minimum than stock shades because the slurry has to be batched specifically and the line flushed when changing color, both of which are downtime. Send a Pantone reference or a physical sample and we produce a match sample before committing to a full run.
The pigment selection decides it, and the requirement varies by market and by food type. Pigments rated for food contact packaging exist across most of the palette, but not all of them. Tell us the market and the application at quotation and we will confirm which shades are available for it rather than assuming the whole range is.
In dark warehouse storage, no. Fading is driven by ultraviolet exposure rather than by time, so stock kept covered holds its shade indefinitely for practical purposes. What causes visible fading is sustained direct sunlight, which affects pale tints first and dark shades last.
Material Name

Farbiger Zellstoff

Material Typ

Individuell gefärbter Zellstoff

Prozess-Kompatibilität

Bonitopak Verpackungsmaterialien

Unsere Verpackungslösungen werden aus nachhaltigen Materialien wie Zuckerrohrfasern, Bambus und recyceltem Zellstoff hergestellt und bieten umweltfreundliche, biologisch abbaubare Optionen für eine Vielzahl von Produkten.

Kompostierbares Kraftpapier ist die festeste Faser, die wir herstellen. Hergestellt aus Frischfaser

Farbiger Zellstoff ist keine eigenständige Faser. Es handelt sich dabei um einen unserer

Gebleichter Zellstoff ist das zu spezifizierende Material, wenn das Bauteil

Der Begriff „natürliche Pflanzenfasern“ umfasst die nicht aus Holz stammenden Zellulosequellen, die wir außerhalb der

Wellpappe als Formmasse bezeichnet wiederverwertete Kartons, die zu Zellstoff zerkleinert wurden

Strohfasern werden aus den nach der Getreideernte übrig gebliebenen Stängeln hergestellt, Material

Unsere Produktkategorien

Entdecken Sie das vielfältige Angebot an Verpackungslösungen von Bonitopak, darunter geformte Zellstoffschalen, Lebensmittelverpackungen, kundenspezifische Designs und nachhaltige Optionen. Jede Kategorie ist auf Langlebigkeit, Funktionalität und Umweltverträglichkeit ausgelegt und auf Ihre spezifischen Anforderungen zugeschnitten.
Sind Sie bereit, Ihr Projekt aufzuwerten?

Erwecken Sie Ihre Entwürfe mit BonitoPak zum Leben

Erleben Sie Präzisionstechnik mit BonitoPak. Von detaillierten Prototypen bis hin zur Großserienproduktion - wir sind da, um Ihre Konzepte in die Realität umzusetzen. Kontaktieren Sie uns noch heute, um Ihre Projektanforderungen zu besprechen!

Verwandte Artikel und Einblicke

Bleiben Sie auf dem Laufenden mit den neuesten Informationen über nachhaltige Verpackungstrends, Einblicke in die Branche und Expertentipps in unserem Blog. Entdecken Sie innovative Ideen und Lösungen, um Ihr Verpackungswissen zu erweitern.

Von Leo Chan | Autor, BonitoPak | Über 20 Jahre Erfahrung im Bereich Verpackungen aus Formzellstoff Wodka ist

Von Leo Chan | Autor, BonitoPak | Über 20 Jahre Erfahrung im Bereich Formzellstoffverpackungen Fast jede

Von Leo Chan | Autor, BonitoPak | Über 20 Jahre Erfahrung im Bereich Verpackungen aus Formzellstoff Hier suchen

Füllen Sie dieses detaillierte Formular aus