 Перейти к содержимому
By Leo Chan | Writer, BonitoPak | 20+ years in molded pulp packaging
The choice between wet pressing vs dry pressing decides four things at once: how your tray looks, how thick its walls are, what the tooling costs, and what each unit costs. Everything else in a molded pulp quote follows from it.
The short answer is simple enough. If your customer sees the tray, look at wet pressing. If the tray is hidden inside a box or carries something rugged, dry pressing does the job for less. The rest of this guide covers the cases where the answer isn’t that obvious.
The Difference in One Table
| Фактор | Сухой прессование | Wet pressing (thermoformed) |
|---|---|---|
| How it dries | Formed, then dried in an oven or dryer | Dried inside heated matched tools |
| Поверхность | One smoother side, one rough, visible fiber | Both faces smooth and dense |
| Typical wall | Thicker | Thinner |
| Detail and draft angles | Softer detail, more draft needed | Fine detail, minimal draft |
| Инструментальная оснастка | Simpler and cheaper | Heated matched tools, more expensive |
| Cycle time | Faster output per line | Slower, limited by the heated press |
| Unit cost | Нижний | Выше |
| Лучшее для | Egg trays, industrial dunnage, seedling trays, hidden inserts | Retail packaging, electronics, cosmetics, anything on display |
What Each Process Actually Does
Both processes start the same way. Recycled paper or plant fiber is pulped with water, and a vacuum pulls that fiber onto a mesh mold shaped like the product.
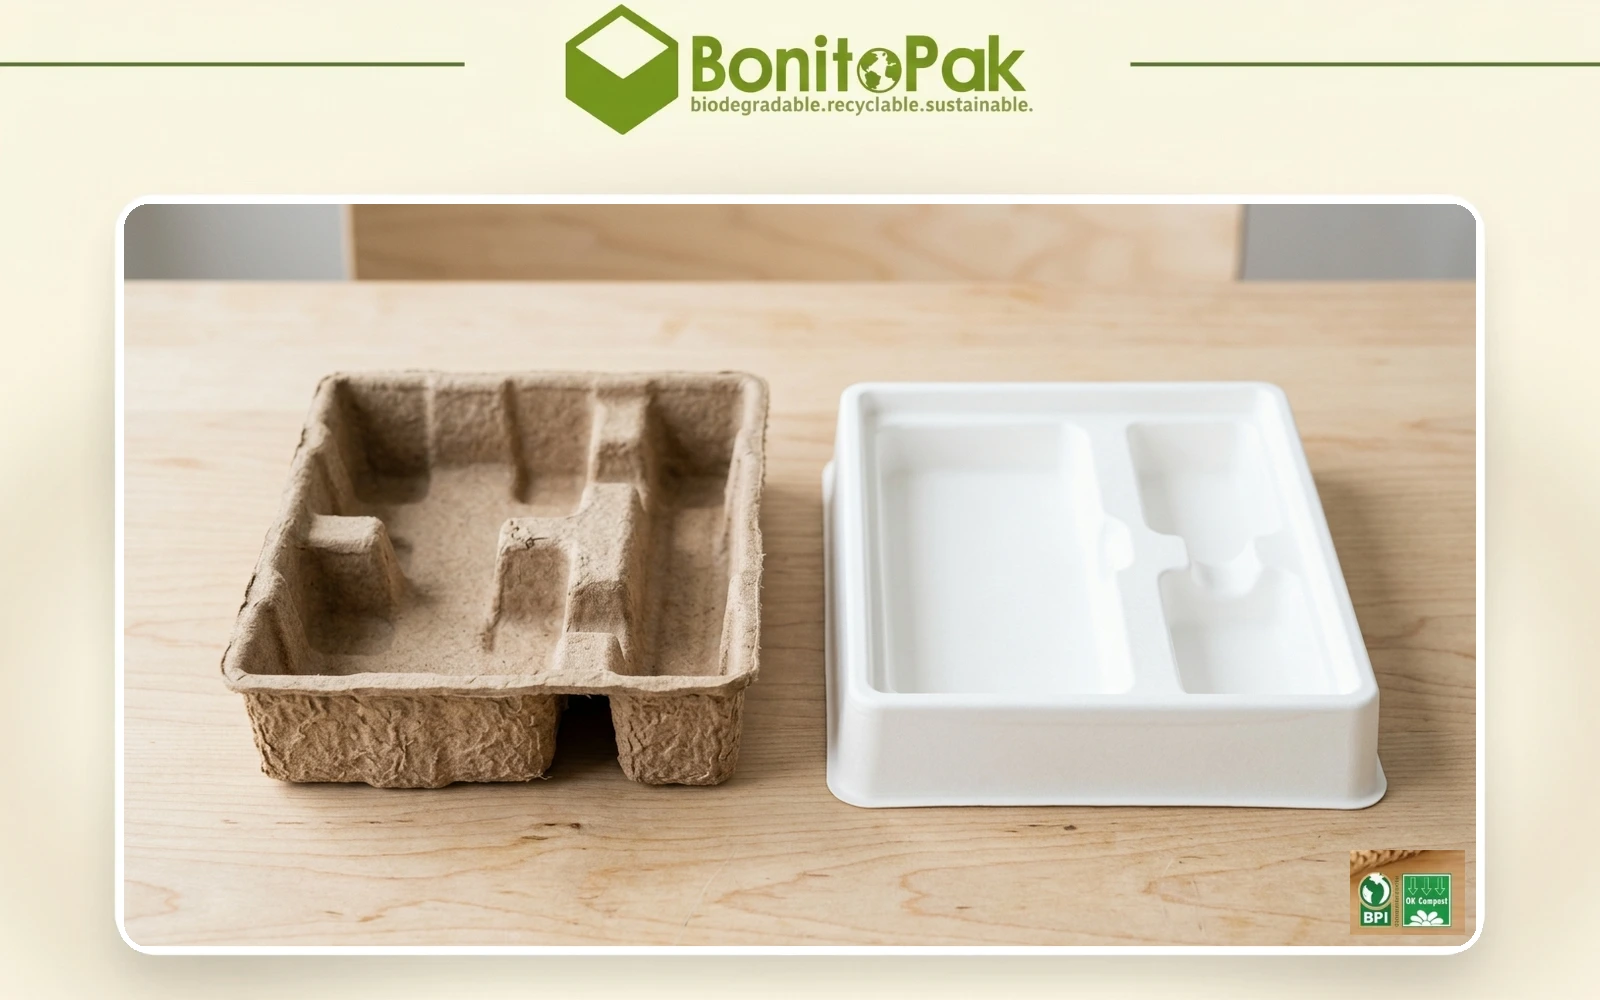
Сухой прессование releases the formed part and dries it afterward, usually in an oven or a multi-layer dryer. Because the part dries unsupported, the walls stay thicker and slightly springy, and the surface keeps the texture of the mesh on one side.
Влажное прессование, often called thermoforming, dries the part between heated tools under pressure. The fiber is compacted while the water leaves, which produces a thin, dense wall with two smooth faces and crisp detail. No separate oven stage is needed.
That single difference, drying inside the tool versus outside it, explains every other item in the table above.
Where the Industry Types Fit In
The International Molded Fiber Association (IMFA) classifies molded fiber into four types, and it’s useful shorthand when you talk to suppliers.
| Тип | Описание | Typical wall thickness |
|---|---|---|
| Type 1 | Thick wall, single mold | About 5 to 10 mm |
| Type 2 | Transfer molded, one forming and one transfer mold | About 3 to 5 mm |
| Type 3 | Thermoformed fiber, multiple heated molds | About 2 to 4 mm |
| Type 4 | Processed, meaning any type with secondary treatment | Варьируется |
Types 1 and 2 are dry pressed territory. Type 3 is wet pressing. Type 4 is whatever you add afterward, such as printing, coating, or die cutting.
Suppliers quote their own achievable ranges, and they’re often tighter than the IMFA bands because equipment and fiber vary. Ask for the range your supplier can actually hold rather than a number from an industry chart. Our article on the 4 типа формованной целлюлозы covers how we apply these categories.
Отделка поверхности
This is what most buyers notice first.
Dry pressed trays show fiber. One face, the one that sat against the mesh, is smoother than the other. In good light you can see the grain. For an egg tray or an industrial insert, nobody minds. For a cosmetics tray sitting in an open gift box, it reads as unfinished.
Wet pressed molded pulp comes out smooth on both faces, with sharper edges and finer definition. They can hold small logos, fine ribs, and tight radii that dry pressing would soften. That finish is also easier to print on and to label cleanly.
If your packaging is opened by a customer, that difference is the whole argument.
Wall Thickness and Protection
Thicker walls absorb more energy. That’s why dry pressed trays suit fragile items that take real handling, including eggs, glassware, and heavy industrial parts. The fiber compresses under impact and recovers.
Wet pressed walls are thinner and denser. They’re strong for their weight and hold their shape well, but there’s less bulk material to absorb a shock. For a light product that needs a premium presentation, that tradeoff is fine. For a heavy product on a rough route, it usually isn’t.
There’s a common mistake worth naming here: choosing wet pressing for packaging nobody sees. You pay for the finish and lose some cushioning at the same time.
Detail, Draft Angles, and Tolerances
Dry pressed parts need more draft, meaning a more generous taper on the walls, so the part releases cleanly and nests properly. Fine text and sharp internal corners come out soft.
Wet pressed parts hold tighter geometry with minimal draft, which matters when the tray has to locate a product precisely. If you’re designing a fitted insert for electronics or cosmetics, this is usually the deciding factor rather than appearance.
Cost: Tooling, Cycle Time, and Unit Price
Three cost effects run in the same direction:
- Tooling. Wet press tooling costs more, because it needs heated matched tools rather than a single forming screen. That’s a one-time charge spread across your volume.
- Cycle time. Heated pressing sets the pace on a wet press line, and each cycle takes time to run. Dry press lines produce far more parts in the same period, which is why they dominate commodity products.
- Unit price. More time per part plus more tooling investment means a higher price per unit at the same volume.
None of that makes wet pressing expensive in a bad way. It makes it a considered choice. If the tray is part of the product experience, the added cost is doing real work. If it isn’t, that spend is invisible to the customer.
Which Process Fits Which Product
| Продукт | Usual process | Why |
|---|---|---|
| Egg trays and cartons | Сухой прессование | Cushioning and cost matter more than finish |
| Industrial and automotive dunnage | Сухой прессование | Heavy parts need thick, springy walls |
| Seedling and nursery trays | Сухой прессование | Function only, high volume |
| Hidden inserts inside a shipper | Сухой прессование | Nobody sees the part |
| Electronics inserts in retail boxes | Влажное прессование | Tight fit, clean presentation |
| Cosmetics and beauty trays | Влажное прессование | Surface finish is part of the product |
| Premium food and gift packaging | Влажное прессование | Smooth faces, printable, shelf facing |
| Bottle and glassware shippers | Either | Depends on whether the pack opens in front of the customer |
Наш сайт Лотки для формованной целлюлозы сухого прессования и Лотки для формованной целлюлозы мокрого прессования pages show typical formats for each, and our molded pulp insert guide covers fitted inserts in more depth.
Fiber Choice Matters as Much as Process
One pairing catches buyers out. Wet pressing recycled paper is a common false economy. Recycled fiber carries a gray base tone, so reaching a clean white or a saturated color over it takes more pigment and more processing, and the finished surface still isn’t as good as bagasse or bamboo would give. If you’re paying for wet pressing, don’t undercut it with the cheapest fiber available.
The reverse also holds. Premium fiber on a dry pressed part that nobody sees is money spent on nothing.
Six Questions That Settle the Choice
- Will the customer see this tray? If yes, lean toward wet pressing.
- How fragile and how heavy is the product? Heavier and more fragile leans toward thicker dry pressed walls.
- How tight does the fit need to be? Precise location leans toward wet pressing.
- What does the surface need to carry? Printing, fine logos, and color hold better on wet pressed faces.
- What is your annual volume? Higher volume absorbs wet press tooling more comfortably.
- What is the tray’s job in the pack? Protection alone points to dry pressing. Presentation plus protection points to wet pressing.
If you’re still split after those six, ask your supplier for samples of the same part in both processes. Handling the two side by side settles it faster than any spec sheet.
Choosing the Process That Matches the Job
Wet pressed molded pulp is worth it when your packaging is part of how the product is experienced. Dry pressed molded pulp is the right default when the tray is doing a job rather than making an impression, and it covers the majority of molded pulp trays produced worldwide, eggs included.
The decision belongs at the start of a project, not at the quote stage, because the process shapes the tooling, and tooling is what you pay for once.
На сайте BonitoPak, we run both wet pressing and dry pressing lines at our Dongguan plant, with in-house mold design and tooling, six pulp colors, and orders from 1,000 pieces. Send us your product and where it will be seen, and we’ll tell you honestly which process it needs.
Часто задаваемые вопросы (FAQ)
Q: What is the main difference between wet pressing vs dry pressing?
A: Where the part dries. Dry pressed parts are formed and then dried outside the tool, giving thicker, rougher walls. Wet pressed parts dry inside heated tools under pressure, giving thin, dense walls and two smooth faces.
Q: Which process is stronger?
A: Neither is simply stronger. Dry pressed walls are thicker and absorb more impact. Wet pressed walls are denser and hold their shape better with less material. Match the process to the load your product actually sees.
Q: Why are egg trays dry pressed?
A: Because cushioning, stacking, and unit cost matter more than surface finish for eggs. Thicker walls protect shells well, and dry press lines produce at the volumes the egg industry needs. Shoppers do not judge egg trays on gloss.
Q: Can dry pressed molded pulp be printed?
A: Yes, though the rougher surface limits fine detail. Embossed logos work well because they need no ink. For sharp printing and small text, wet pressing or a printed label or sleeve is the better route.
Q: Does wet pressing always cost more?
A: For the same part, usually yes, through both tooling and cycle time. The gap narrows at high volume as tooling is spread across more units. Ask for both quotes at your real annual volume before deciding.
 Russian
 English
 German
 Spanish
 French
 Japanese
 Portuguese
 Arabic